
How Does a VFD Save Energy? Energy Saving Principle Explained
Industrial electric motors can consume a significant amount of electricity, especially in pumps, fans, blowers, compressors, conveyors, and other continuously operating equipment. For applications where motor speed changes according to actual process demand, operating a motor at full speed all the time can result in unnecessary energy consumption.
A Variable Frequency Drive (VFD) can help reduce this energy consumption by adjusting motor speed according to the actual load requirement.
But how does a VFD save energy?
The basic principle is simple:
A VFD reduces energy consumption by allowing an AC motor to operate at the speed required by the application instead of continuously running at full speed.
This can be particularly effective for centrifugal pumps, fans, and blowers, where power consumption decreases rapidly as motor speed is reduced.
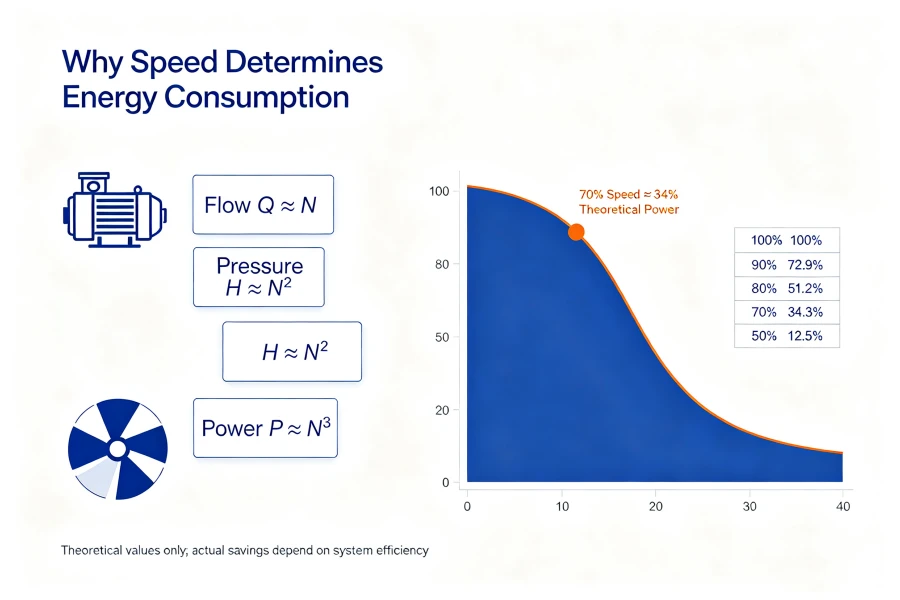
For example, under ideal affinity-law conditions, operating a pump or fan at 70% speed requires approximately 34% of the theoretical power at 100% speed.
This guide explains how VFD energy saving works, why motor speed has such a significant effect on power consumption, which applications benefit most, and how engineers can evaluate a VFD energy-saving project.
How Does a VFD Save Energy?
A VFD saves energy primarily through variable-speed motor control.
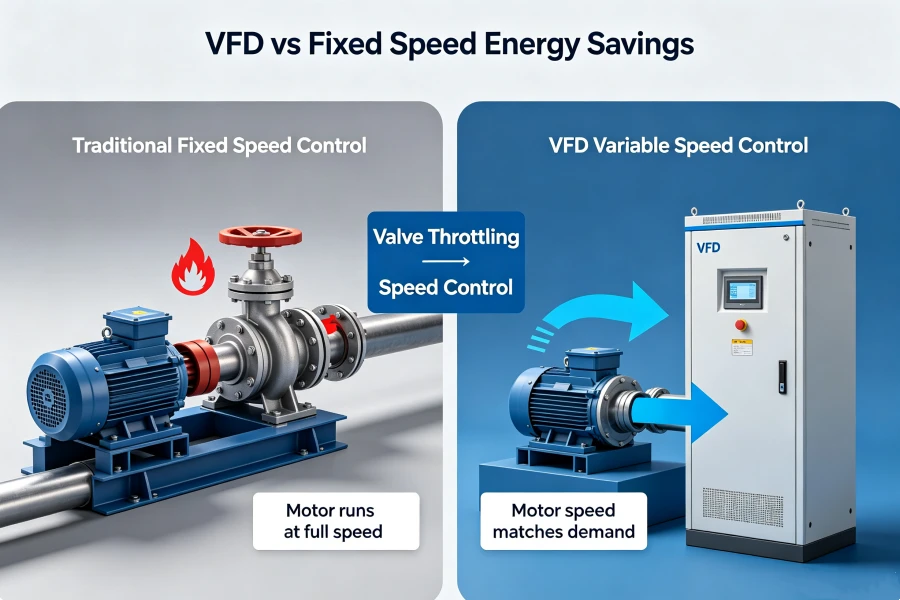
Traditional motor systems often operate at a fixed speed. When the process requires less flow, pressure, or airflow, the system may use a valve, damper, bypass, or other mechanical method to reduce the output.
For example:
Fixed-Speed Motor → Pump → Valve → Process
The motor may continue operating at full speed even when the system only requires part of its maximum capacity.
A VFD changes this approach:
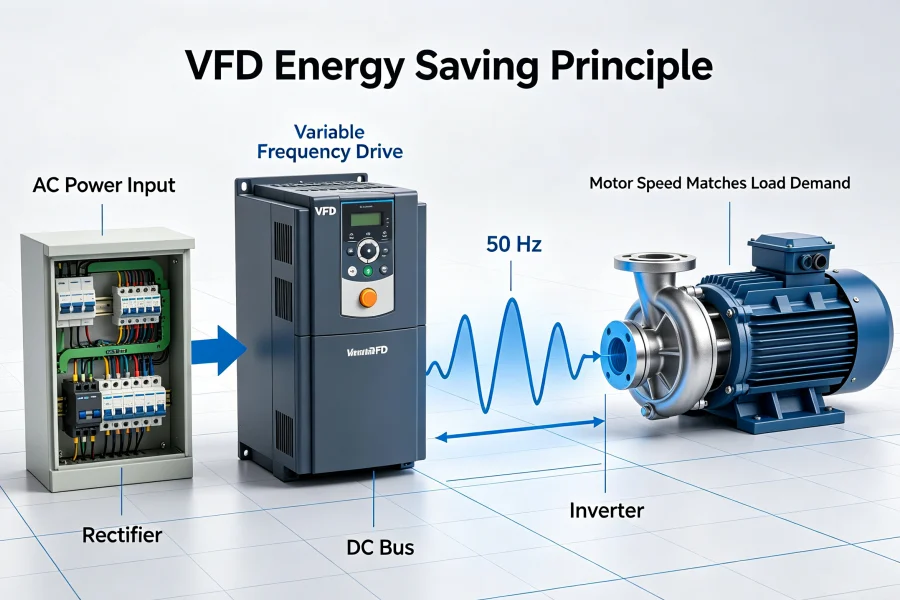
AC Power → VFD → Variable-Speed Motor → Pump → Process
Instead of restricting the output while the motor continues running at full speed, the VFD reduces motor speed to match the actual process demand.
For example:
50 Hz → Full Speed
40 Hz → Reduced Speed
35 Hz → Further Reduced Speed
30 Hz → Low-Speed Operation
The motor therefore produces only the output required by the application.
This is the fundamental principle behind VFD energy saving.
Learn More:VFD vs Soft Starter vs DOL Starter: Which Motor Control Method Is Best?
Why Motor Speed Has Such a Large Impact on Energy Consumption
The energy-saving potential of a VFD becomes particularly significant when the motor drives a variable-torque load, such as a centrifugal pump or fan.
For these applications, engineers commonly use the fan and pump affinity laws to understand the relationship between motor speed, flow, pressure, and power.
The simplified relationships are:
Flow
Q ∝ N
Flow is approximately proportional to motor speed.
Pressure or Head
H ∝ N²
Pressure or pump head is approximately proportional to the square of motor speed.
Power
P ∝ N³
Power is approximately proportional to the cube of motor speed.
The third relationship is especially important for energy optimization.
Because power is related approximately to the cube of speed, a relatively small reduction in speed can result in a much larger reduction in theoretical power requirement.
Why Does 70% Speed Use About 34% Power?
This is one of the most important concepts when evaluating VFD energy savings for pumps and fans.
Using the simplified affinity-law relationship:
Power Ratio ≈ Speed Ratio³
At 70% speed:
Power Ratio = 0.70³
Power Ratio = 0.343
Therefore:
70% speed ≈ 34.3% of theoretical power requirement
A simplified comparison is:
| Motor Speed | Theoretical Power Requirement |
|---|---|
| 100% | 100% |
| 90% | 72.9% |
| 80% | 51.2% |
| 70% | 34.3% |
| 60% | 21.6% |
| 50% | 12.5% |
This explains why VFDs can provide substantial energy-saving potential in variable-flow pump and fan applications.
However, these values represent the theoretical affinity-law relationship under suitable conditions. Actual energy consumption will vary depending on motor efficiency, VFD losses, pump or fan efficiency, system resistance, static pressure, mechanical losses, operating point, and other system characteristics.
Therefore, engineers should not assume that every system operating at 70% speed will consume exactly 34% of its original electrical power.
Read More:Industrial VFD Applications: Pumps, Fans, Compressors and Automation Systems
VFD Energy Saving vs Traditional Fixed-Speed Control
Consider a conventional pump system.
The pump motor operates at full speed, while a valve is used to control the required flow.
The simplified system is:
Motor → Pump → Valve → Process
If the process requires less flow, the valve partially closes.
The motor, however, may still operate close to its original speed.
With VFD control:
Motor → Pump → Variable Speed → Process
The VFD reduces motor speed according to the required flow.
This can reduce the power required by the pump system.
| Control Method | Motor Speed | Flow Control | Energy-Saving Potential |
|---|---|---|---|
| DOL + Valve | Mostly constant | Throttling | Low |
| Fixed Speed + Damper | Mostly constant | Damper control | Low |
| Soft Starter | Mostly constant | Limited | Low |
| VFD | Variable | Speed control | High potential |
The important distinction is that a soft starter primarily improves the starting process, while a VFD can continuously adjust the motor’s operating speed.
Which Applications Benefit Most from VFD Energy Saving?
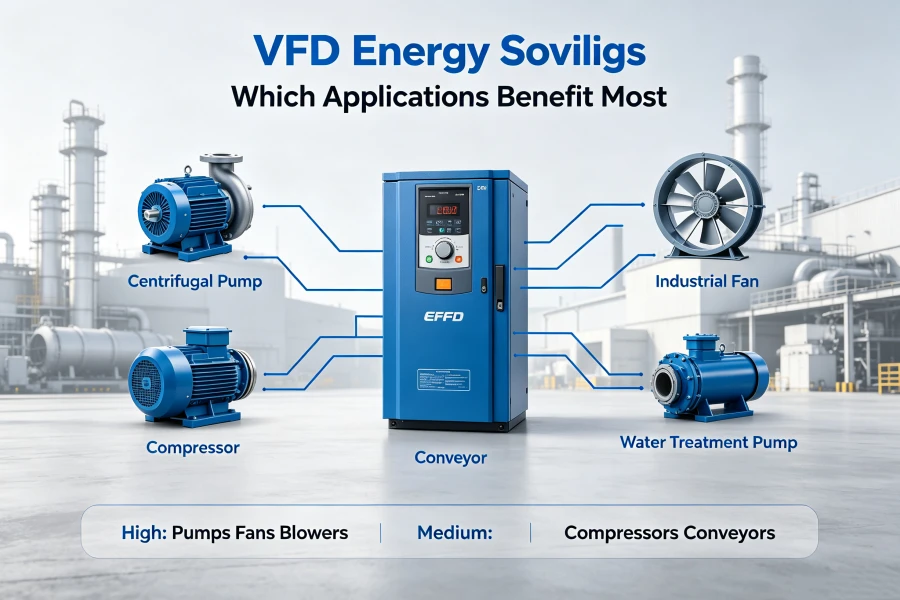
Not every motor application has the same energy-saving potential.
VFDs are particularly effective when the required output changes over time and the motor can safely operate at different speeds.
Centrifugal Pumps
Centrifugal pumps are one of the most common applications for VFD energy optimization.
Typical applications include:
- Water supply
- Booster pumps
- HVAC circulation
- Industrial process water
- Irrigation
- Cooling water
- Water treatment
- Wastewater systems
Instead of running a pump continuously at full speed, a VFD can adjust speed according to:
- Flow demand
- Pressure
- Tank level
- System temperature
- Process requirements
For example, a large pump may require full speed during peak demand but operate at reduced speed during periods of lower demand.
Industrial Fans and Blowers
Industrial fans and blowers can also benefit significantly from variable-speed control.
Typical applications include:
- HVAC systems
- Factory ventilation
- Exhaust systems
- Cooling towers
- Dust collection
- Industrial air handling
- Process ventilation
Instead of operating the fan continuously at maximum speed and restricting airflow with a damper, a VFD can adjust fan speed according to the actual airflow requirement.
Compressors
VFDs can also be used for variable-demand compressor systems.
Depending on the compressor design and control strategy, motor speed can be adjusted according to actual air or gas demand.
Potential benefits include:
- Reduced unloaded operation
- Improved pressure control
- Reduced starting stress
- Better matching of motor output to demand
However, compressor applications require careful analysis because the energy-saving characteristics depend heavily on compressor type, control method, pressure requirements, and operating profile.
Conveyors
Conveyors are often considered constant-torque applications rather than classic affinity-law applications.
A VFD can still provide important benefits through:
- Adjustable conveyor speed
- Smooth acceleration
- Controlled deceleration
- Reduced mechanical shock
- Process synchronization
However, the energy-saving potential may not be as dramatic as with centrifugal pumps and fans.
Read More:Industrial Power Quality Problems and Solutions: Transformer, AVR, SVG and AHF
Does a VFD Always Save Energy?
No.
Installing a VFD does not automatically guarantee significant energy savings.
The energy-saving potential depends mainly on the load type and operating profile.
VFDs generally provide strong energy-saving opportunities when:
- Motor speed can be reduced
- Process demand varies
- The load is suitable for variable-speed operation
- The motor operates for long periods
- The existing system relies on throttling or damping
- The motor frequently operates below maximum capacity
For example, centrifugal pumps and fans are often strong candidates for VFD energy optimization.
On the other hand, energy savings may be limited when:
- The motor always needs full speed
- The load requires constant power
- The process cannot tolerate speed reduction
- The motor is already operating efficiently at the required speed
- The equipment operates only for short periods
Therefore, the correct question is not:
“Will a VFD save energy?”
It is:
“Can the motor speed be reduced while still delivering the required process output?”
If the answer is yes, there may be a strong opportunity for energy optimization.
Variable Frequency Drive Efficiency: Does the VFD Consume Energy?
A VFD is not 100% efficient.
The power electronics inside the drive create some electrical losses during operation.
These losses can occur in:
- Rectifier components
- DC bus components
- Switching devices
- Inverter section
- Cooling fans
- Internal control electronics
Therefore, the VFD itself consumes some power.
However, the energy-saving benefit can still be much greater than the VFD’s internal losses when the drive significantly reduces motor speed in a suitable application.
For example, reducing a centrifugal pump from full speed to a lower operating speed can reduce the mechanical power required by the pump much more significantly than the additional losses introduced by the VFD.
This is why engineers should evaluate system-level efficiency, rather than looking only at the VFD’s own efficiency rating.
How Much Energy Can a VFD Save?
There is no single percentage that applies to every VFD installation.
Actual energy savings depend on:
- Motor power
- Motor efficiency
- VFD efficiency
- Operating hours
- Average operating speed
- Load type
- Existing control method
- Pump or fan efficiency
- System resistance
- Electricity cost
A simple starting point for an energy calculation is:
Energy Consumption (kWh) = Power (kW) × Operating Hours
Annual energy savings can then be estimated by comparing the original system with the VFD-controlled system.
Annual Energy Saving = Original Energy Consumption − VFD System Energy Consumption
The financial benefit can be estimated as:
Annual Energy Cost Saving = Energy Saved × Electricity Price
For a detailed industrial project, engineers should use actual operating data rather than relying only on theoretical affinity-law calculations.
Example: 315kW VFD Energy Saving Application
Consider a 315kW industrial pump motor operating for approximately 6,000 hours per year.
Suppose the application frequently operates below its maximum flow requirement.
If the pump can safely operate at approximately 70% speed during part of the operating period, the theoretical affinity-law relationship suggests:
70% speed → approximately 34.3% theoretical power requirement
However, this does not mean the actual electrical consumption will automatically become exactly 34.3% of the original value.
A proper engineering calculation should also consider:
- Motor efficiency
- VFD efficiency
- Pump efficiency
- Static head
- System curve
- Minimum flow requirements
- Actual operating speed
- Operating hours at each speed
- Hydraulic losses
This type of analysis can determine whether a VFD retrofit provides an attractive return on investment.
For larger industrial equipment, VFD solutions in the 315kW to 500kW range can be considered for suitable pumps, fans, blowers, compressors, conveyors, and other industrial motor applications.
How to Select a VFD for Energy Optimization
Choosing the correct VFD is important for achieving reliable operation and energy performance.
1. Motor Power
Start with the motor nameplate rating, such as:
- 315kW
- 400kW
- 500kW
However, motor power alone is not enough.
2. Motor Rated Current
The VFD should be selected according to the motor’s rated current and the required application duty.
VFD selection should not be based on motor kW alone.
The actual motor current is particularly important for high-power applications.
3. Input Voltage
Common industrial voltage configurations include:
- 380V
- 400V
- 415V
- 440V
- 460V
- 480V
The selected VFD must match the electrical system and motor requirements.
4. Frequency
Typical industrial systems operate at:
50Hz or 60Hz
The required operating frequency and speed range should be determined from the application.
5. Load Type
Determine whether the application is:
- Variable torque
- Constant torque
- Heavy duty
- Constant power
This directly affects VFD sizing and overload requirements.
6. Required Speed Range
Determine the minimum and maximum motor speed required by the process.
For example:
30–50Hz
or
20–60Hz
The motor, cooling system, mechanical equipment, and process must all be suitable for the selected speed range.
7. Overload Capacity
Applications such as conveyors, compressors, crushers, and heavy industrial machinery may require greater overload capacity than typical variable-torque pump or fan applications.
Learn More:How to Select a VFD for an AC Motor? Complete Sizing Guide
When Should You Use a VFD for Energy Saving?
The following table provides a simplified guide.
| Application | VFD Energy-Saving Potential | Main Benefit |
|---|---|---|
| Centrifugal Pump | High | Variable flow and pressure |
| HVAC Pump | High | Variable circulation demand |
| Industrial Fan | High | Variable airflow |
| Blower | High | Variable air demand |
| Water Treatment Pump | High | Flow and pressure control |
| Compressor | Medium / High | Variable demand |
| Conveyor | Medium | Speed and process control |
| Crusher | Low / Medium | Speed and torque control |
| Constant-Speed Motor | Low | Limited opportunity for speed reduction |